Home/Manufacturing

Made on the Sunny Side of the Alps.
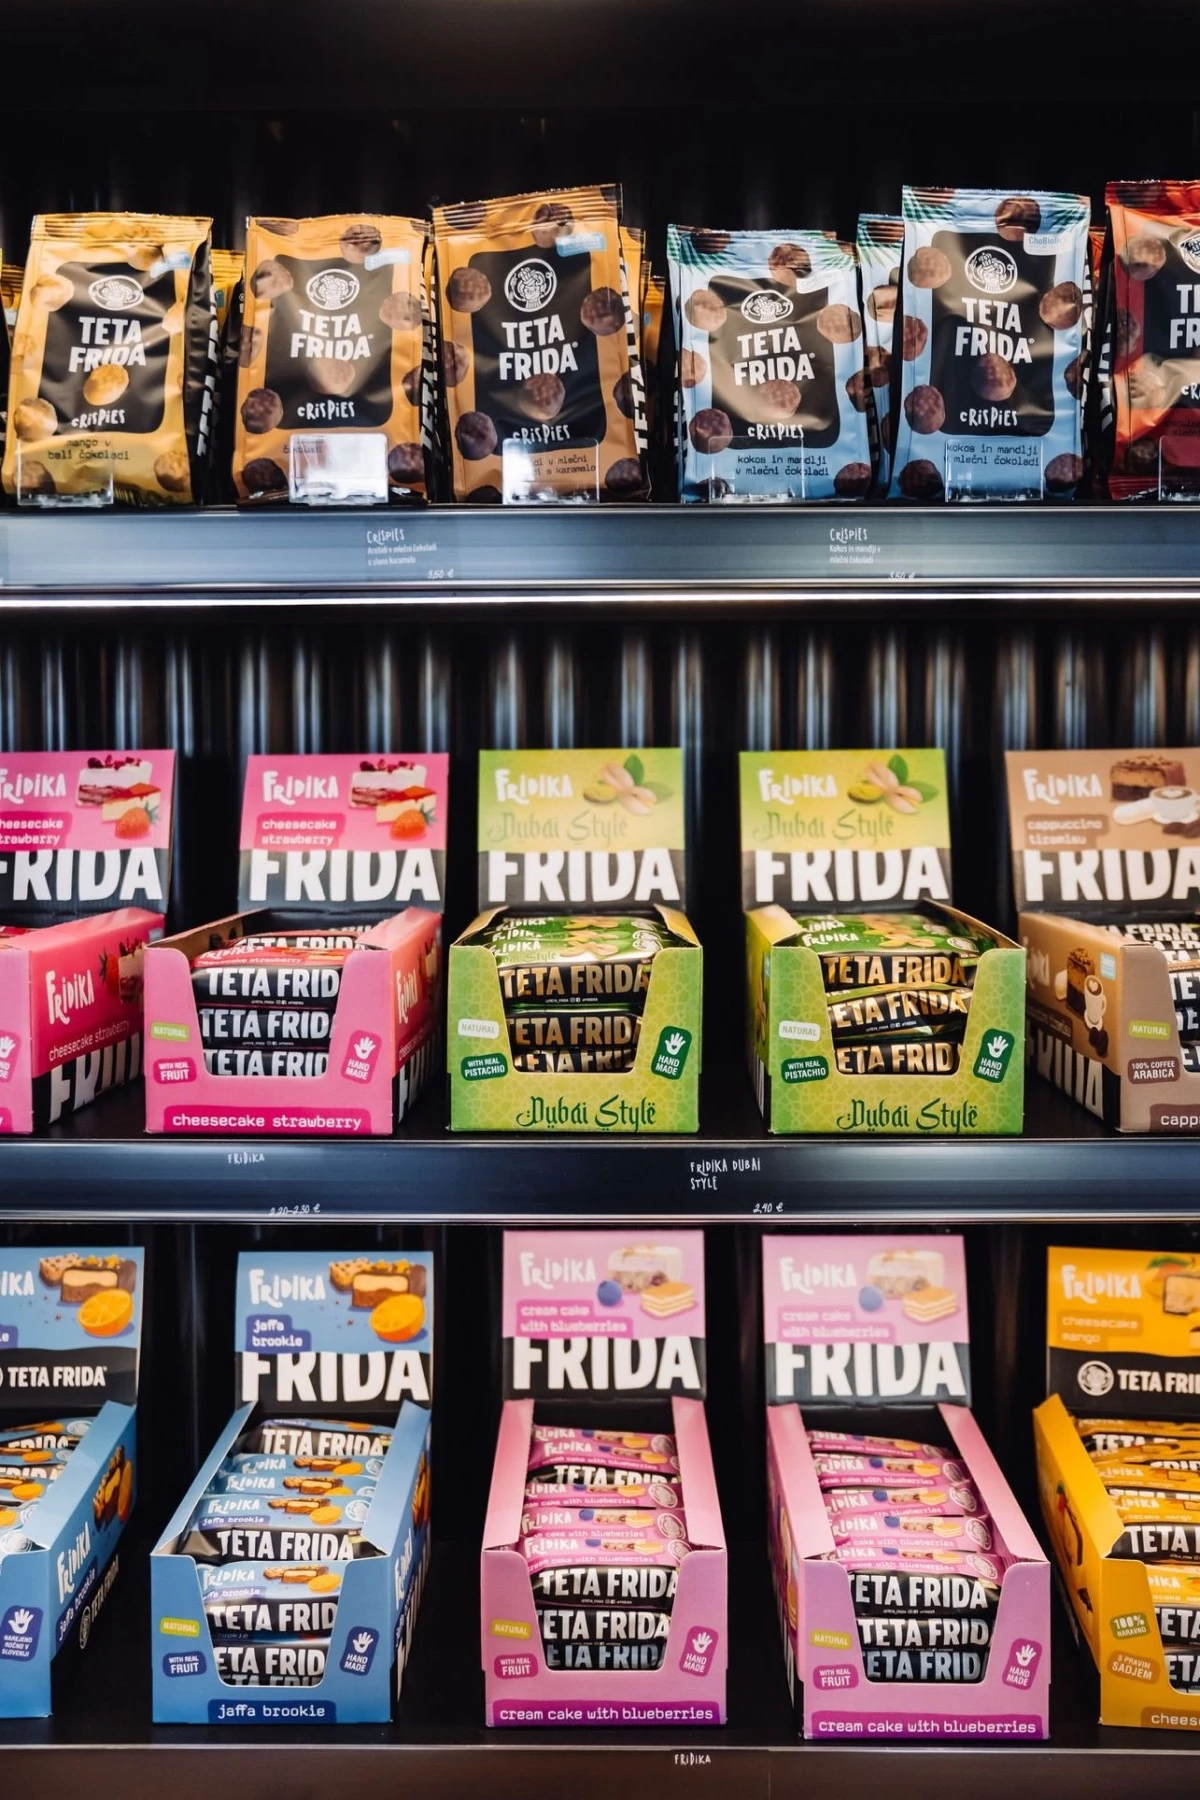
Proven on shelves worldwide.

One roof for development, production, packaging and logistics. Modern lines, our own R&D and a certified food-safety system, built for private label and for our own brands.

What we do

Everything under one roof.

From the first sketch to the pallet leaving Maribor, every step is handled by our own team.

Own Product Development

From idea to finished product.

Private Label Expertise

Flexible solutions tailored to your market.

Modern Production

State-of-the-art manufacturing and quality control.

Packaging Development

Innovative packaging concepts and shelf-ready solutions.

Fast Market Response

Efficient development and production processes.

International Experience

Trusted by leading retailers across Europe and beyond.

Trusted by leading retailers

Our products sit on the shelves of Europe's biggest retail chains, drugstores and petrol networks.

As a private label manufacturer we work behind the scenes for some of the most demanding buyers in Europe. The same lines, the same quality system and the same team are available for your brand.

Manufacturing

Manufactured
With Purpose.

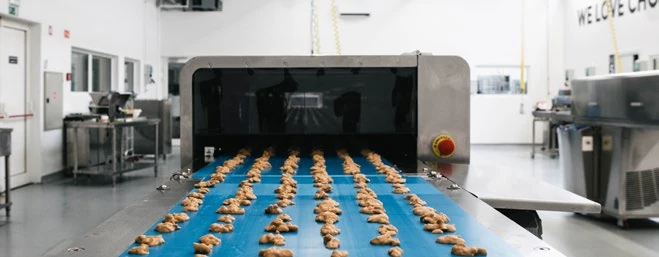
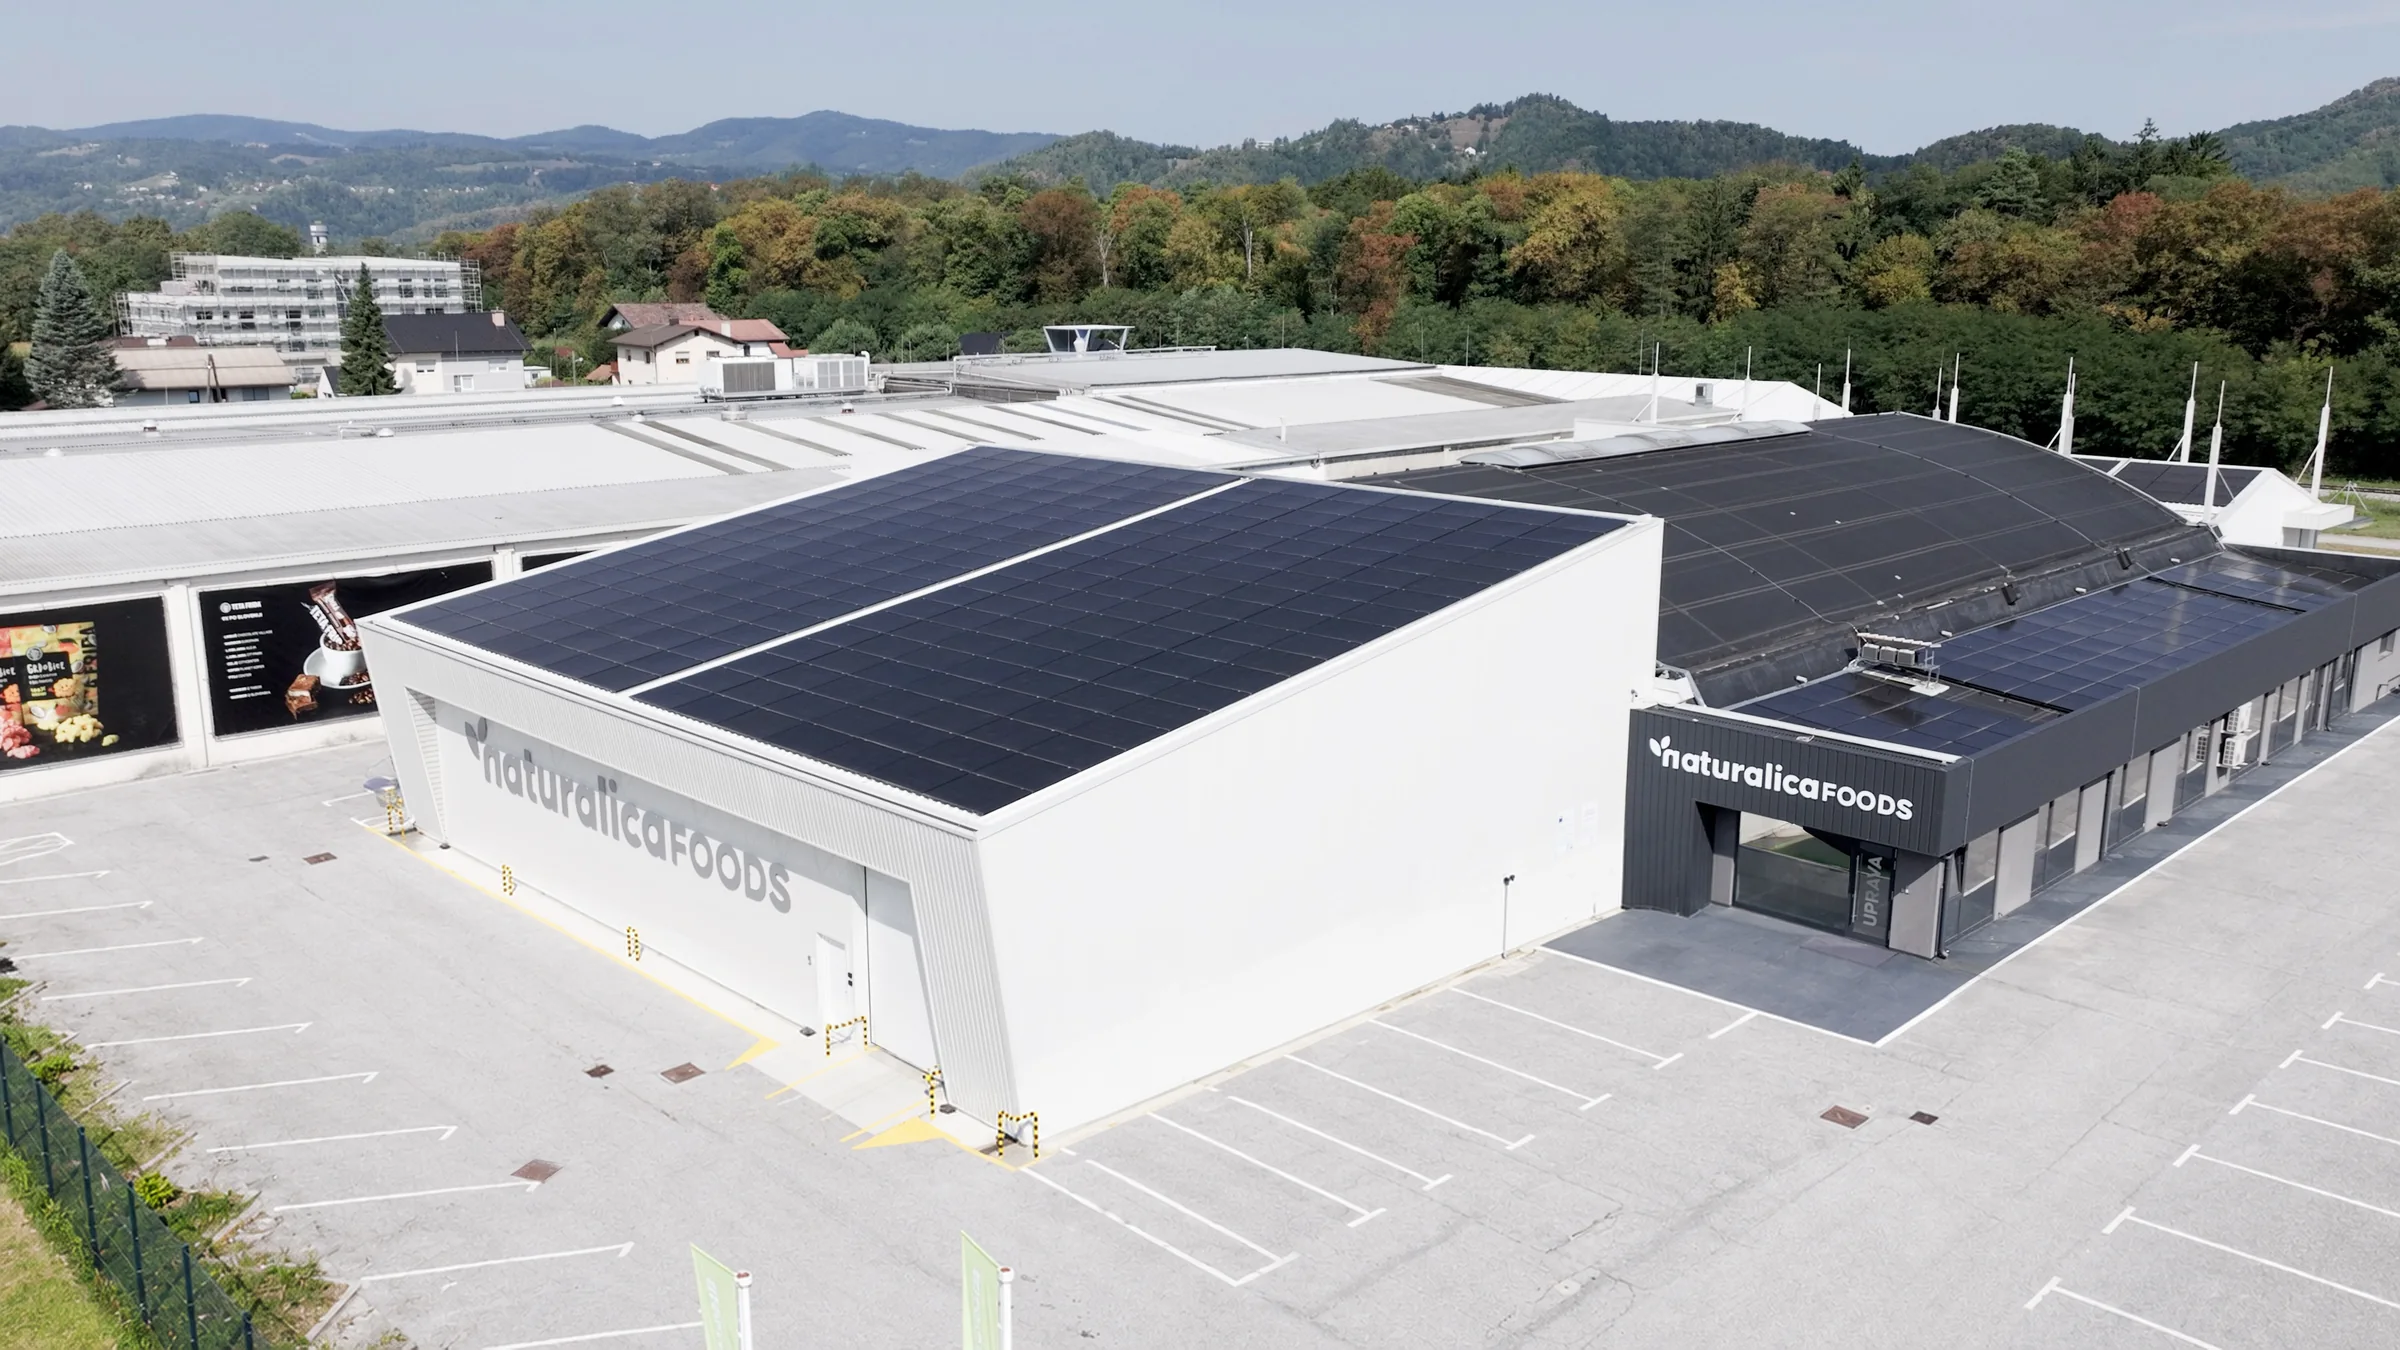
State-of-the-art facilities, advanced technology and strict quality standards ensure exceptional products, every time. Our plant runs on a solar roof with battery storage, sustainable by design.

Naturalica Foods production facility in Maribor, seen from above
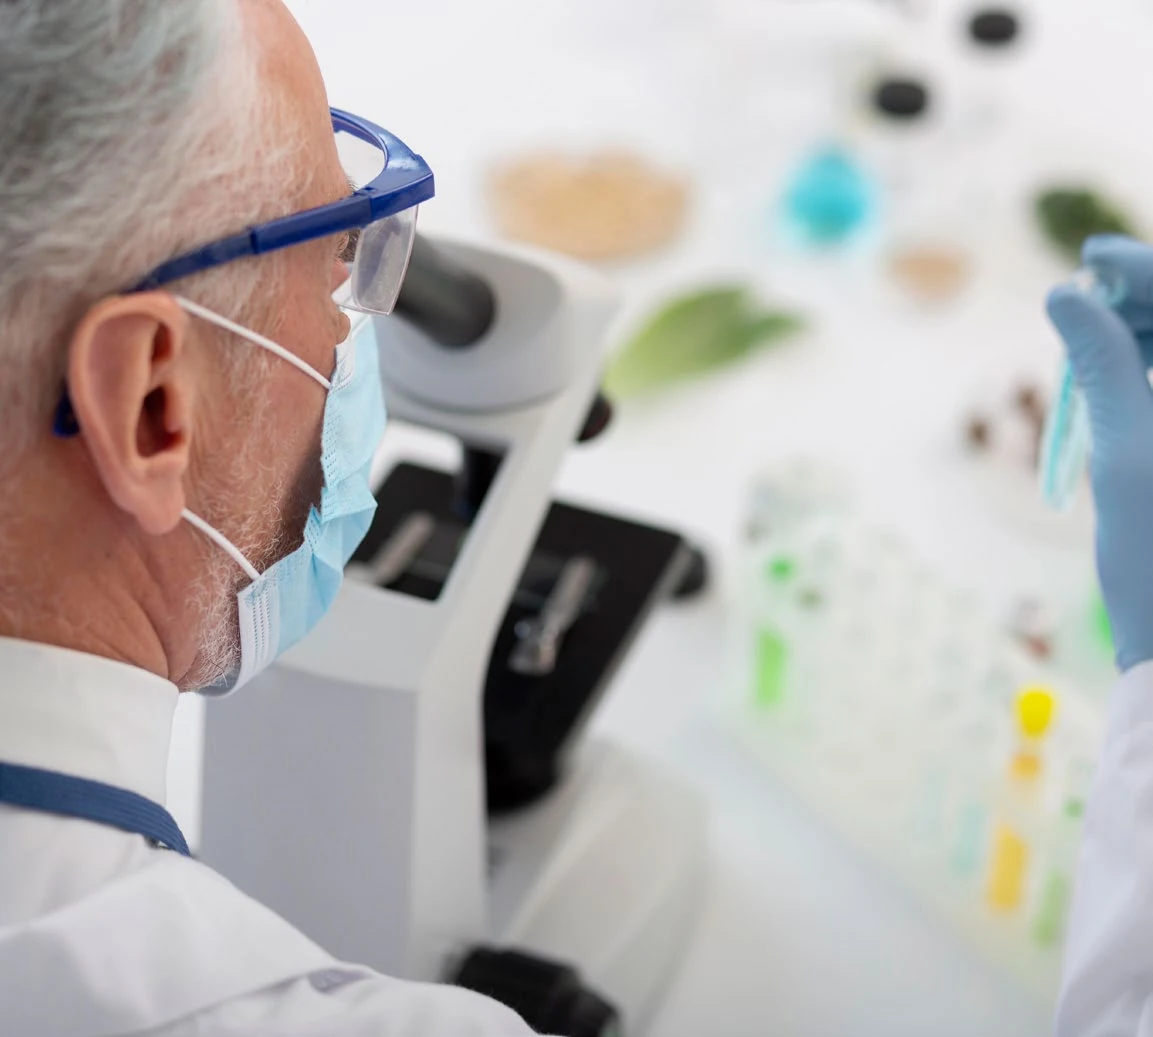
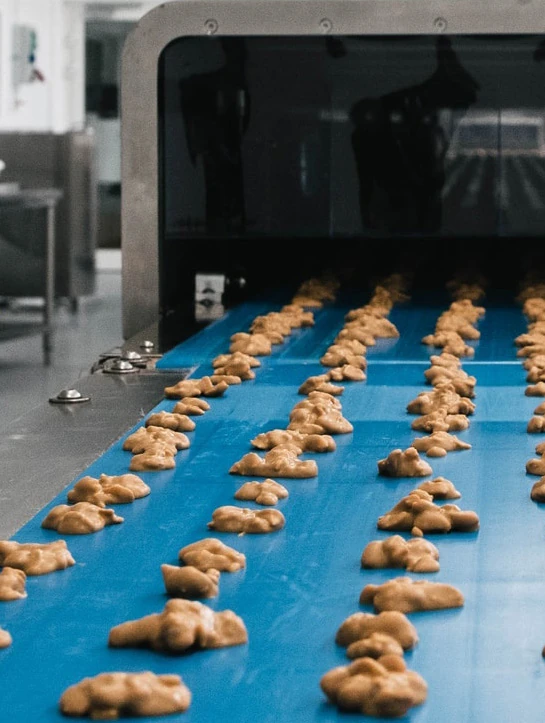
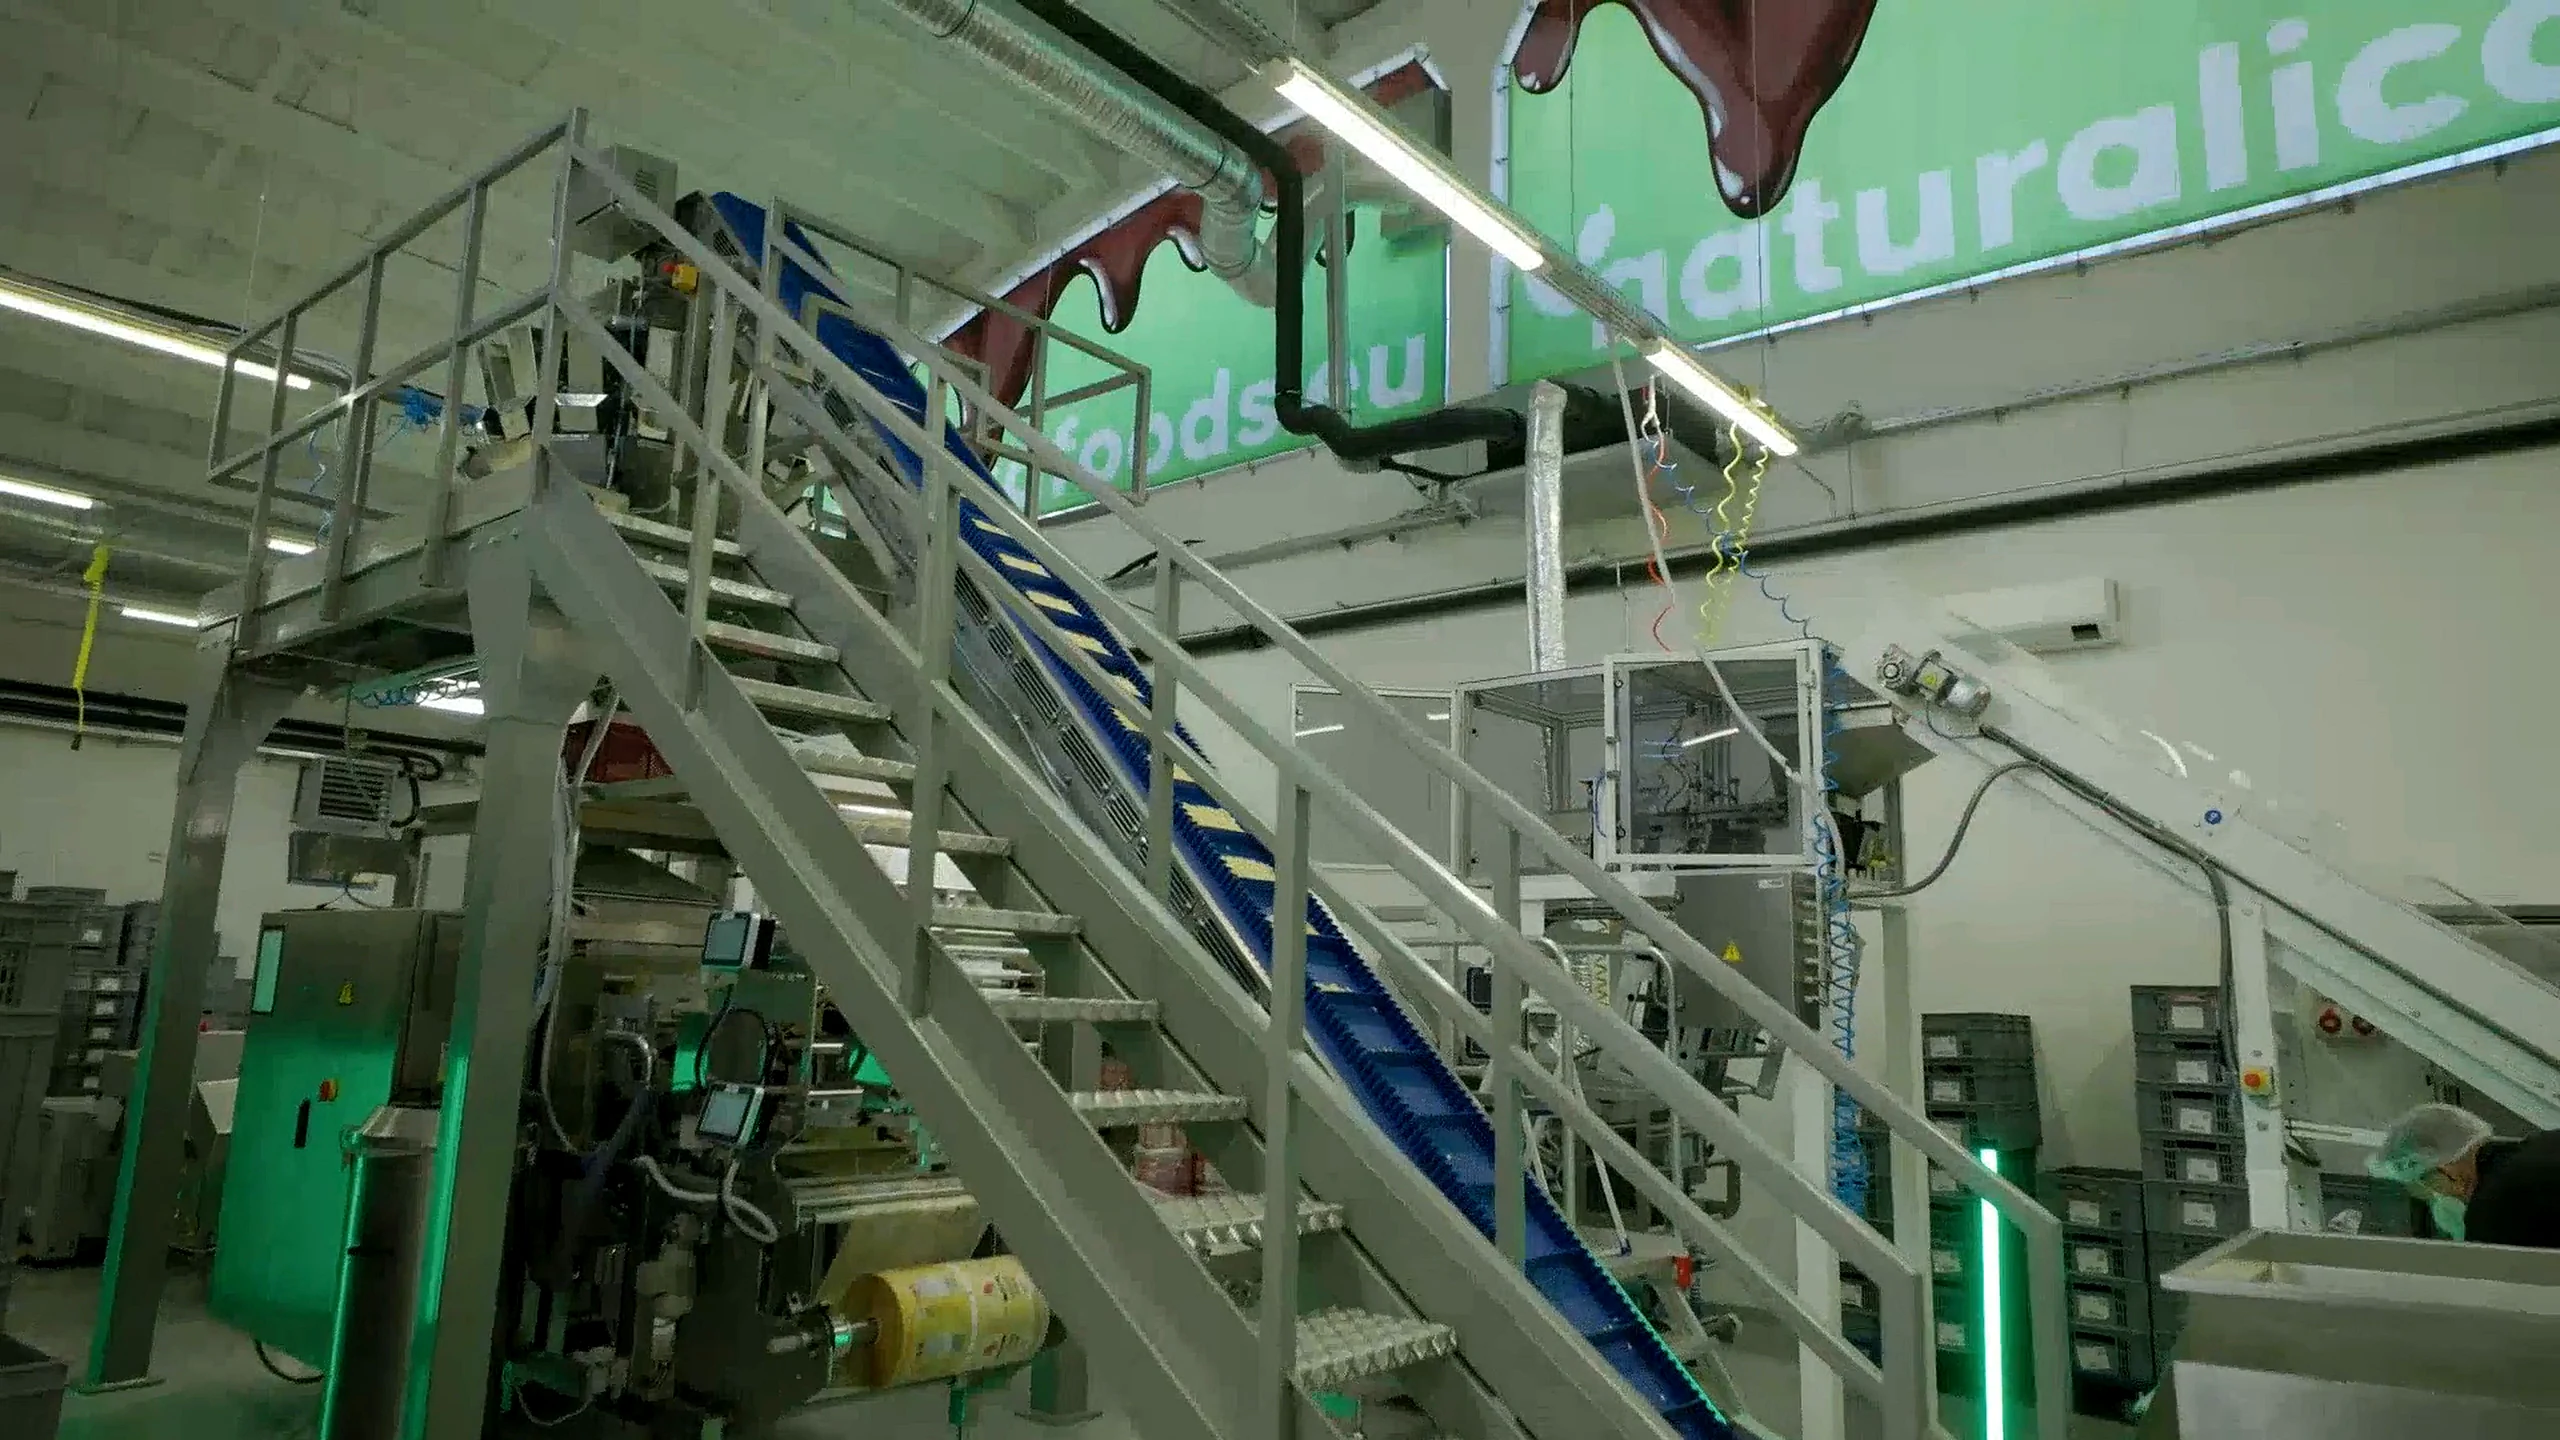
Chocolate production line Quality control in the Naturalica lab
IFS Food certified ISO certified Halal certified Kosher certified
Naturalica Foods production facility · Maribor, Slovenia
Research & development

Where chocolate meets science.

Next-generation functional chocolate: premium products enriched with live probiotic cultures and multivitamins, developed in our own R&D department and produced under a certified food-safety system.

Own R&D departmentFrom concept to tasting sample
Live probiotic culturesStable inside the finished product
Multivitamin conceptsHair & nails, cognition, wellbeing
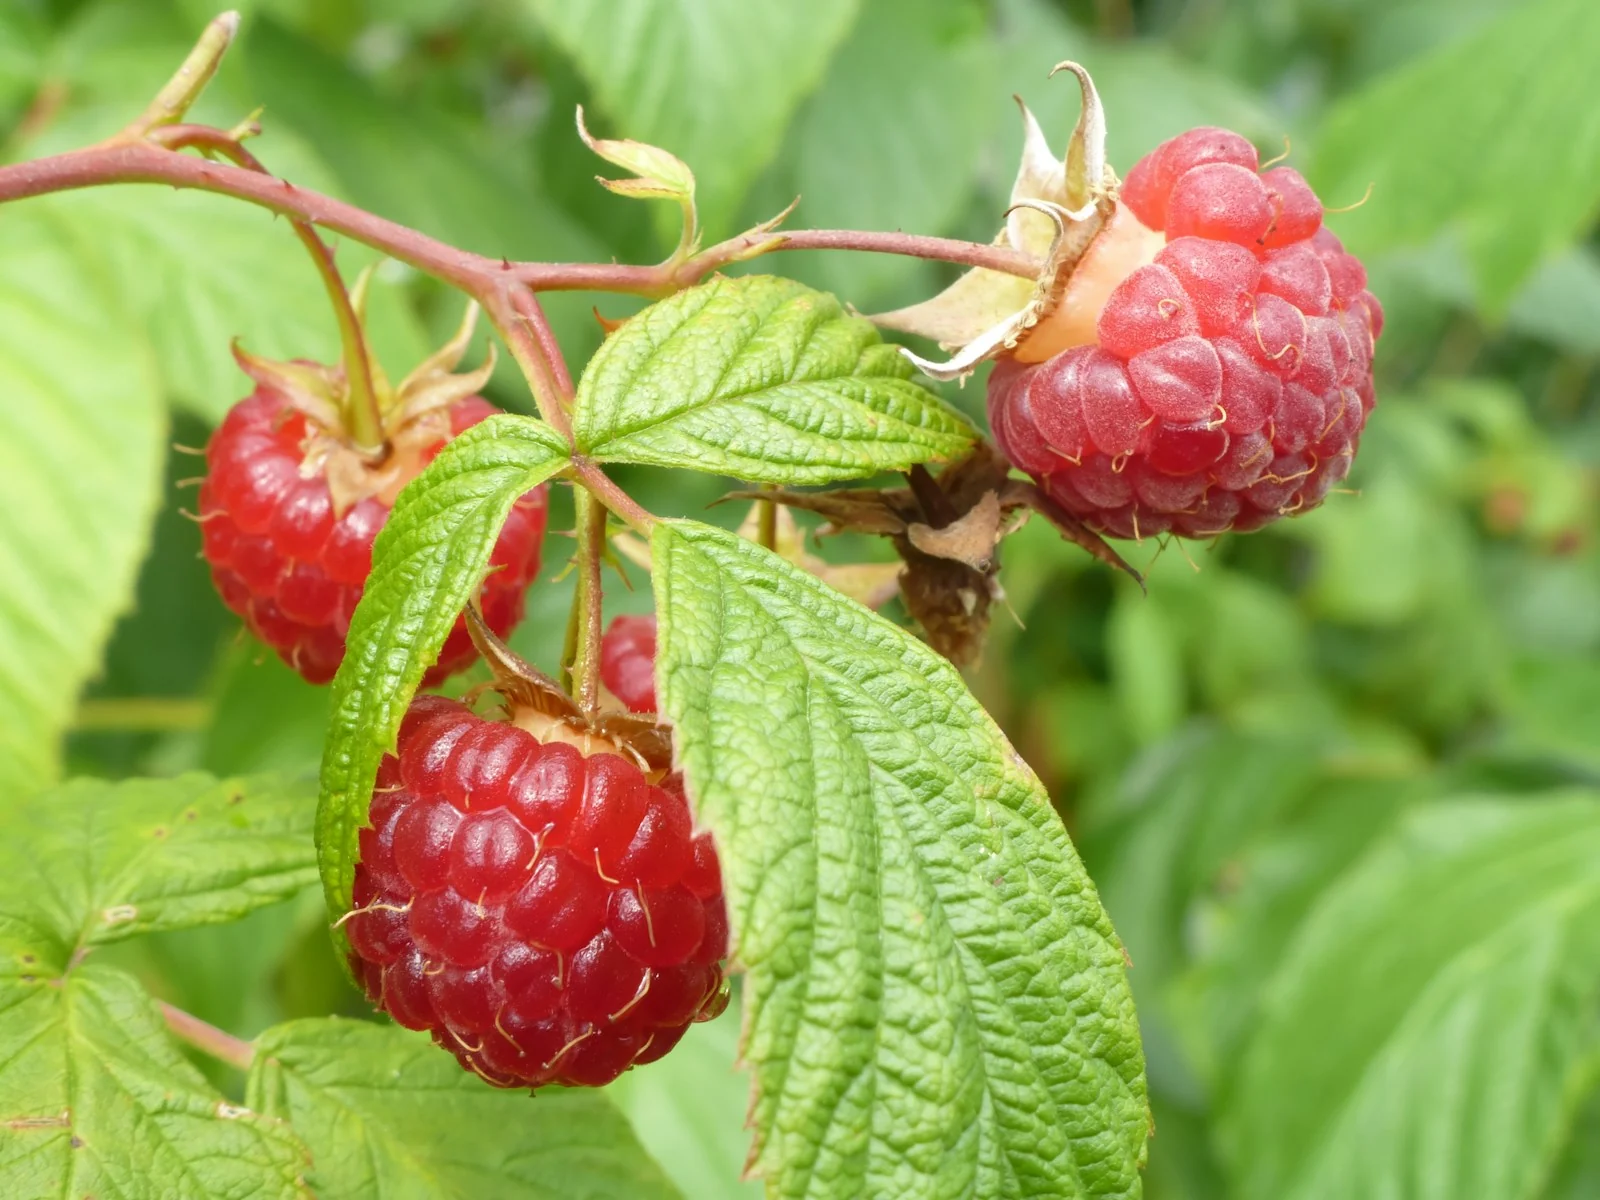
European fruit, no palm oilWillamette raspberries, Senga Sengana strawberries
Our process

From concept to consumer.

We handle every step of the journey, so our partners can bring great products to market faster.

01

Idea & Research

Trend scouting, concept sketches and recipe ideas, shaped together with our partners.

Idea & Research
02

Product Development

Our own R&D team turns concepts into recipes, prototypes and tasting samples.

Product Development
03

Manufacturing

Production on modern lines under IFS Food, ISO 14001, Halal and Kosher standards.

Manufacturing
04

Packaging Design

In-house designers create shelf-ready packaging, from doypacks to retail displays.

Packaging Design
05

Market Validation

Sensory panels, retail tests and partner feedback before we scale up.

Market Validation
06

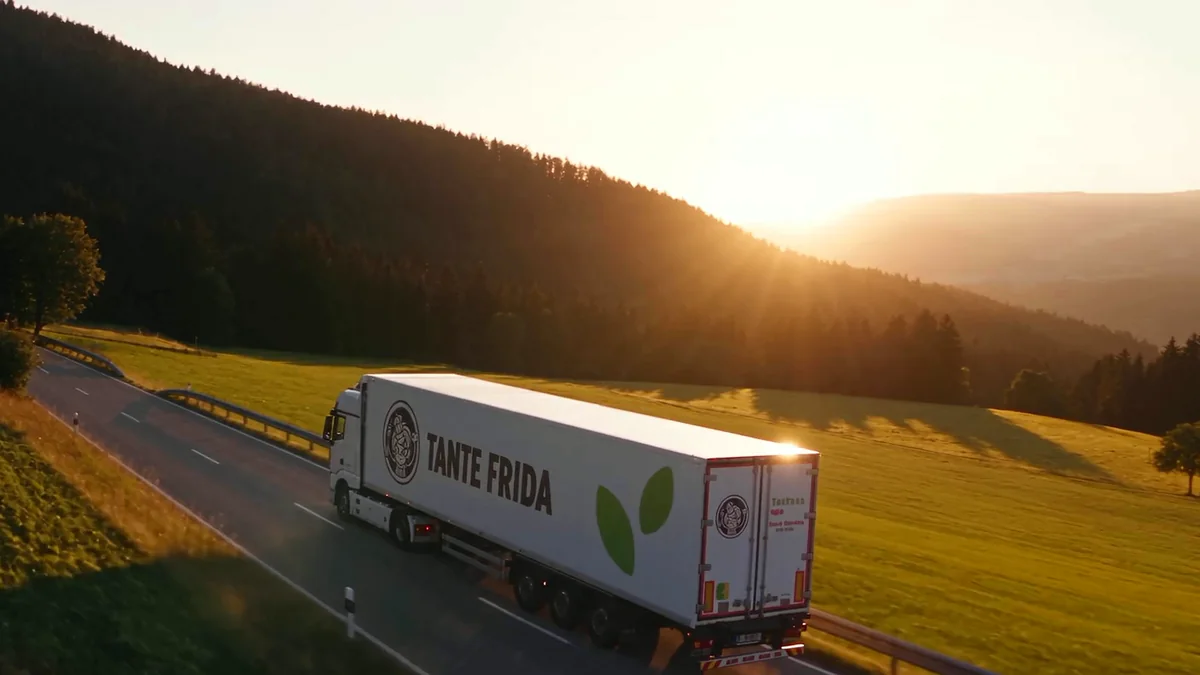
International Distribution

From our warehouse in Maribor to shelves in more than 25 countries.

International Distribution
100% natural ingredients

No compromises.
Only real ingredients.

Every product starts with whole fruit and real Belgian chocolate. Nothing artificial, nothing hidden.

  • Premium Belgian chocolate: 100% cocoa butter, no artificial glazing agents
  • No palm oil: no shea butter, no coconut fat
  • 100% European raspberries & strawberries: with geographical certification: only Willamette raspberries and Senga Sengana strawberries
  • No added sugar: only naturally occurring sugars
  • Low-temperature processing: preserves vitamins, minerals and natural flavours
  • Natural taste and colour
Quality & certifications

Rigorous quality, certified.

We assign the highest priority to rigorous quality management. Our strict food safety system ensures compliance with all legal requirements and guarantees an uninterrupted chain of inspections and documentation for each stage of the production process.

IFS Food certified ISO 14001 Halal certified Kosher certified AAA Platinum credit rating Rainforest Alliance

Let's Build Something Together.